If you’ve ever walked through a chemical processing plant, a water treatment facility, or even a large-scale food and beverage production line, you’ve likely passed dozens of gate valves without giving them a second thought. These unassuming components are the unsung workhorses of fluid control, regulating the flow of everything from corrosive acids to potable water. Today, I want to break down one of the most common types we supply here at our gate valve business: the non-rising stem gate valve. Over the years I’ve worked with valves, I’ve seen how the right choice here prevents downtime, leaks, and even costly safety hazards, so I’m sharing what every plant manager, maintenance tech, and project engineer needs to know about this workhorse. Gate Valve
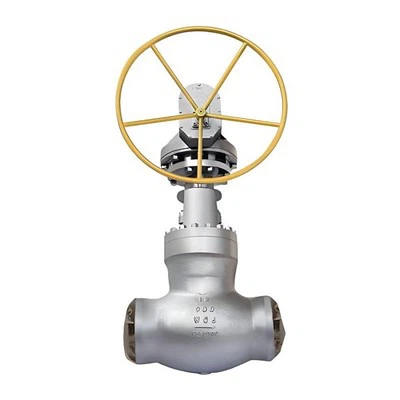
First, let’s start with the basics. A gate valve, in general, operates by lifting a solid metal gate (the part that actually blocks or allows fluid flow) up and down inside the valve body. The gate slides perpendicular to the direction of the flow, which is why it’s called a gate—like a gate in a fence opening and closing to control access. Now, the key difference between a non-rising stem gate valve and its counterpart, the rising stem gate valve, is what happens to the stem (the long metal rod you turn when you operate the valve) when you open or close it. With a rising stem gate valve, the stem itself extends upward out of the valve body as you open it, so you can physically see how open or closed the valve is just by looking at the height of the stem above the handwheel. A non-rising stem gate valve, as the name hints, doesn’t do that— the stem stays flush or almost flush with the top of the valve body when you operate it, so you can’t tell its position just by looking. That might sound like a small detail, but it changes everything about where and how you use this valve.
Let me explain how it works mechanically, because that’s where it gets practical. Inside the non-rising stem gate valve, the stem has threads cut into it that only go partway down, usually inside the valve body. When you turn the handwheel, those threads engage with a fixed nut mounted in the top of the valve body, so instead of the stem moving up and down, it rotates, which pulls the gate up or down along the stem’s threads. So the entire operating mechanism is tucked inside the valve housing, right next to the gate, rather than extending above it. That compact design is the main reason our customers come back for non-rising stem gate valve time and time again.
Now, before I get into use cases, I should clear up a common misconception I hear all the time: non-rising stem gate valves are less reliable than rising stem ones. That’s not true—they’re just designed for different conditions. The rising stem is ideal when you need to visually confirm position, like in a critical pipeline where you can’t afford to accidentally leave a valve partially open or closed. But non-rising stems shine in spaces where height is limited, or where the valve is buried underground or in a tight mechanical room. I once had a customer at a municipal water district call me in a panic because their rising stem valves on a buried main were getting damaged by heavy construction equipment above ground— the extending stems were sticking up too high, and a backhoe had sheared off three of them. We replaced those with non-rising stem gate valves, and they haven’t had an issue in five years. That’s the kind of real-world problem this valve solves.
Another key advantage of non-rising stem gate valves is their durability in dirty or corrosive environments. Because the stem doesn’t extend out of the valve body, there’s no exposed thread or stem to collect debris, sludge, or chemicals. A rising stem’s upper threads are exposed, so over time, grime can build up there, making the handwheel hard to turn, or even causing the stem to seize up. The non-rising stem keeps all the moving parts sealed inside the valve, protecting them from the elements. For example, in a pulp and paper mill where there’s constant exposure to wood chips, black liquor, and other viscous byproducts, non-rising stem gate valves hold up way longer than exposed stem valves. I’ve also supplied these valves for use in mining slurry lines, where abrasive solids would scratch exposed stems and cause leaks—our non-rising models eliminate that risk.
Now, let’s talk about limitations, because no valve is perfect, and I don’t want to mislead anyone. First, you can’t visually check the open/closed position without adding an external indicator, which is an extra component we can supply, but something to plan for. If position clarity is critical—say, in a nuclear power plant cooling system or a pharmaceutical manufacturing line—you’ll want to add a stem position monitor, or opt for a rising stem. Second, non-rising stem gate valves generally require more torque to operate, especially when the valve is large or is part of a high-pressure line. The threads are fully enclosed, so there’s more friction between the stem and the nut when turning, which means you might need a larger handwheel, a gear operator, or even an actuator for electric or pneumatic operation. That’s a tradeoff, of course, for the compact size. Third, these valves aren’t ideal for frequent operation. They’re designed for on/off service, not throttling flow—if you try to adjust the gate partially open all the time, the edges of the gate will erode faster, leading to leaks. Stick to opening them fully or closing them completely, and they’ll last for decades.
Let’s break down the most common applications I see our non-rising stem gate valves used for, to give you a sense of when this is the right choice. Buried underground pipelines, as I mentioned earlier, are a top use case. Municipal water and sewer systems, oil and gas distribution lines, and utility transmission lines all rely on these valves because their low profile doesn’t interfere with excavation, paving, or other work around the lines. They’re also great for aboveground installations in tight mechanical rooms or skids, where there’s limited vertical space—like in a ship’s engine room, where every inch of headroom counts, or in a modular process skid for small chemical plants.
Another big one is low-pressure, non-critical service lines. For example, in the food and beverage industry, breweries and wineries use non-rising stem gate valves for water intake lines, waste lines, and low-pressure transfer lines. They work well here because they’re easy to clean (the sealed mechanism means less crevice for bacteria to hide) and their compact size fits in tight brewery layouts. We also supply them for HVAC systems in large commercial buildings, where they control water flow to heating and cooling coils—again, the low profile is perfect for the tight ceilings and mechanical rooms common in office towers and hospitals.
Now, a note on materials, because that’s what makes a valve compatible with your specific fluid. Non-rising stem gate valves come in all kinds of materials, and as a supplier, we work with our customers to pick the right one for their application. For potable water lines, we usually offer ductile iron bodies with EPDM seals or stainless steel for extra corrosion resistance. For oil and gas lines, carbon steel or cast steel bodies handle high pressure and hydrocarbons, and for corrosive chemical lines, we have options in alloy 20, Hastelloy, and PVC for low-pressure, non-abrasive chemicals. The stem is almost always stainless steel, because it needs to resist rust and wear from repeated operation, even if it’s enclosed.
I’ve had countless customers ask me: “Should I choose a rising or non-rising stem gate valve?” The answer almost always comes down to two factors: space and position visibility. If you have plenty of headroom and need to be 100% certain the valve is open or closed at a glance, go with rising. If you’re working in a tight space, dealing with buried lines, or need a valve that holds up to dirty, abrasive environments, non-rising is the way to go. I always tell people to factor in maintenance, too—non-rising stem gate valves require less regular cleaning of external parts, since there’s no exposed stem to wipe down. That’s a big win for facilities with high turnover maintenance teams, or teams that are stretched thin.
Let me share a quick story to illustrate that. A client at a regional wastewater treatment plant reached out to me two years ago, saying their maintenance team was spending 10 hours a week just cleaning and lubricating their rising stem valves on the plant’s raw sewage lines. The exposed stems were getting caked in grease, grit, and sewage, making them impossible to turn after a few years, and the team was often late turning valves off during maintenance, leading to unplanned overflows. We replaced 12 of their worst valves with non-rising stem gate valves, and they reported back that maintenance time for those valves dropped to less than an hour a month. No more grit in the threads, no more seized stems, and no more missed valve turns. That’s the kind of impact choosing the right valve can have on your operations.
Another point to consider is operation. Non-rising stem gate valves can be manual, operated by a handwheel, or automated with electric, pneumatic, or hydraulic actuators. Since they don’t have an extending stem, actuating them is simpler, because you don’t have to account for vertical movement of the stem— the actuator just needs to turn the handwheel shaft, which is much easier to integrate into automated control systems. That’s why they’re often the go-to valve for industrial automation projects, where you need to control dozens of valves remotely.
Now, let’s cover a few key things to look for when selecting a non-rising stem gate valve, to avoid common pitfalls. First, make sure you pick the correct pressure rating for your application. Non-rising stem gate valves come in pressure classes like 150, 300, 600, and higher, so if you’re working on a high-pressure oil line, a 150-class valve won’t cut it—you’ll need a 300 or higher. Second, confirm the end connections: they can be threaded, flanged, or wafer-style, depending on how you’re connecting the valve to your pipeline. Third, if position visibility is a concern, invest in a external position indicator or a limit switch, so your control room can tell at a glance if the valve is open or closed. I’ve seen too many projects where people buy a cheap non-rising valve without a position indicator, and end up with months of downtime because no one could confirm the valve was closed for maintenance.
As a gate valve supplier, I’ve built my business on helping customers navigate these choices, because I know that picking the wrong valve isn’t just an inconvenience—it can lead to leaks, safety hazards, and lost production. Last year, we had a customer in a small chemical plant try to save money by buying a generic non-rising stem gate valve for a line carrying 150 PSI of hydrochloric acid. The valve they bought was only rated for 100 PSI, and it failed after six months, causing a small leak that had to shut down the entire plant for three days. We replaced that valve with a custom-sized, acid-resistant non-rising stem gate valve, and that plant hasn’t had an issue since. That’s the reason I take the time to talk through every detail with each customer: it’s not just selling a valve, it’s ensuring your operation runs smoothly.
At the end of the day, the non-rising stem gate valve is a versatile, durable component that solves specific problems that other valves can’t. It’s not the right valve for every application, but when it is, it’s irreplaceable. Its compact design, resistance to debris, and ease of automation make it the top choice for buried lines, tight mechanical spaces, and dirty or abrasive environments. If you’re working on a project right now and aren’t sure if a non-rising stem gate valve is the right fit, or if you need help selecting the right size, material, or pressure rating, reach out to our team of valve experts. We can walk through your specific application, answer any questions you have, and help you find the perfect valve for your needs.

Don’t let a bad valve choice slow down your operations or create unnecessary costs. Get in touch with our team today to discuss your gate valve requirements, and we’ll help you find a reliable, long-lasting solution that fits your space, pressure, and fluid needs.
Check Valve References:
- Miller, J. (2020). Industrial Valve Technology: A Guide to Selection and Application. Industrial Press.
- American Water Works Association. (2018). Valve Selection and Installation for Water and Wastewater Systems. AWWA Manual M17.
- Karassik, I. J., Messina, J. P., Cooper, P., & Heald, C. C. (2007). Pump Handbook (4th ed.). McGraw-Hill.
- Fluid Controls Institute. (2019). Valve Types and Applications: A Comprehensive Overview. FCI Technical Bulletin 101.
- National Fire Protection Association. (2021). Standard for Fire Protection in Industrial Processes (NFPA 88A).
Wuxi PYNOS Flow-tech Co., Ltd.
As one of the leading gate valve manufacturers and suppliers in China, we offer a wide range of products with superior quality. We warmly welcome you to buy high quality gate valve made in China here from our factory. We also accept customized orders.
Address: Sales Center: 7th Floor, No.19 Qingyuan RD, Wuxi City, Jiangsu Prov., China
E-mail: Info@pynosvalve.com
WebSite: https://www.pynosvalves.com/
